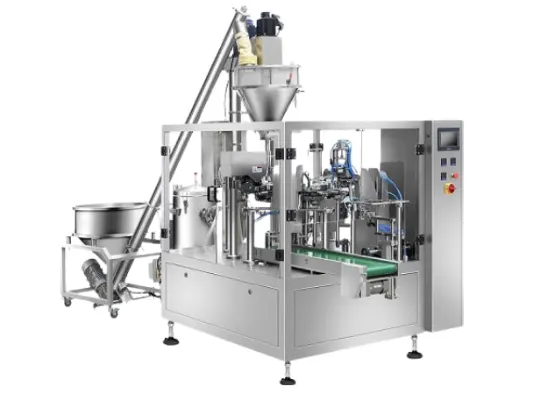
It has been noted that the shisha molasses has a high content of glycerin, honey, and volatile flavors. The sealing process of the shisha pack is important for ensuring shelf life, odor retention, and preventing leakage during transportation. It is a fact that even the tiniest gap in the seal of the packaging would cause oxygen to penetrate into the packaging and result in evaporation of moisture and quick oxidation of the initial flavoring. Modern shisha production facilities increasingly use Premade Pouch Shisha Packaging Machines to automate pouch picking, opening, filling, and sealing operations. But getting a perfect, 100% airtight seal is a task that can be accomplished only with proper calibration of several operational parameters.
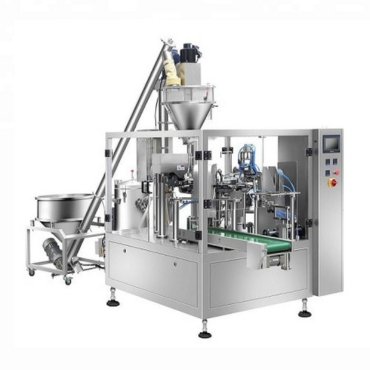
1. Core Factors Affecting Sealing Quality in a Premade Pouch Shisha Packaging Machine
A consistent, tight, and airtight seal requires accurate thermal energy, balanced mechanical force, consistent materials, and an absolutely clean sealing surface.
1.1 Sealing Temperature
The thermal energy will cause melting of the specially designed inner sealant layer (usually PE or CPP) of the laminated barrier films, which allows polymer chains to bond together when cooled down.
Low Temperatures: In the case of low sealant temperature, the seal layers cannot melt enough to create a homogeneous polymer bond. As a result, the seal strength is far below the 15 N/15 mm industrial threshold, making pouches prone to leaking.
High Temperatures: If too much heat is supplied, it will simply burn the thin laminated film (PET/AL/PE), shrink the plastic film, and damage the outer artwork and the aluminum barrier layer.
Sealing Temperature Range: The standard multilayer shisha pouches typically have seal temperatures set between 130°C and 180°C, depending on the thickness of the film (80 to 150 μm).
1.2 Sealing Pressure
It is the mechanical compression process that ensures the squeezing out of any air bubbles existing between different layers of film during the melting of the inner plastic.
- Insufficient force: Minute gaps will exist because of wrinkles or folds, or gussets around the opening of the bag.
- Excessive force: The melted plastic flows sideways outside the main sealing area and results in a very thin sealed portion with a weak seam.
- Settings recommended: The pneumatic seal system employed in the Premade Pouch Shisha Packaging Machine operates well at an air pressure level ranging from 0.3MPa to 0.6MPa.
1.3 Dwell Time of the Seal
Transfer of heat through heavy aluminum foil or through multi-layer laminate takes some dwell time. In high-speed production processes, dwell time usually varies from 0.5 to 1.5 seconds. If the Premade Pouch Shisha Packaging Machine is running above its designed capacity, then the dwell time decreases below 0.3 seconds, and heat does not penetrate completely despite correct operation of heat block sensors.
1.4 Pouch Material & Quality
Inconsistency in the pre-made pouches leads to unexpected sealing problems that equipment can fail to address. Differences in film thickness of more than ±10% result in non-uniform heat penetration for various production batches. Pinholes in the thin aluminum layer or a defective solventless gluing process further affect airtightness. Additionally, structural differences among stand-up pouches, flat sachets, shaped bags, and zipper pouches require flexible machine jaw configurations.
1.5 Product Contamination
The viscosity of the molasses is very high (3,000-5,000 cPs), which makes the molasses sticky to the parts made of stainless steel used in the machinery. While the volumetric or multi-head weighing fill machine operates at high speed, small droplets of the molasses or tobacco fibers occasionally land on the inner seal portion of the pouch openings. Organic particles between the sealing jaws do not allow plastic films to seal properly, and seal strength reduces by more than 50%, leading to instantaneous fruit juice leakage.
In order to prevent this problem of contamination, the machinery manufacturers, for example ShishaPack, use special servo cut-off nozzles, positive air cleaning devices, and mechanical shields isolating the sealing zone during the filling process.
1.6 Machine Condition & Wear of Parts
Jaw alignment, spring balance, and surface conditions determine the temperature and pressure distributions across the width of the package. If there is carbonized sugar, worn silicone bands, or misaligned jaws by more than 0.05 mm, the package develops cold spots that are prone to pressure testing.
| Impact Factor | Failure Symptom | Recommended Parameter / Solution |
| Temperature fluctuations | Poor sealing or scorched film | Use PID temperature control to maintain variations within ±1°C. |
| Unbalanced Pressure | Single-sided leaks, thin seams | Calibrate dual pneumatic cylinders; keep pressure at 0.3–0.6 MPa |
| Product Splatter | Contaminated seal, pouch rupture | Use anti-drip dosing nozzles and air-jet mouth cleaners |
| Jaw Surface Wear | Faded seal pattern, channel leaks | Clean jaws daily with brass brushes; check mechanical parallelism monthly |
2.Improving Performance and Troubleshooting a Premade Pouch Shisha Packaging Machine
Zero defects in packaging cannot be maintained on a busy, multi-shift production line without process control, calibration, and maintenance processes:
Establishing a Stable Process Window for Sealing
When switching pouch suppliers and pouch material thickness, do tensile and burst testing in a wide range of temperatures, pressures, and times to find the widest, most tolerant window of stability.
Install Post-Fill Cleaning and Inspection
Install pouch stretch-out claws, top blow-out dust equipment, and double seal points before heat sealing. Contemporary Premade Pouch Shisha Packaging Machine usually includes additional press bars, seal area inspection sensors, and automatic vision reject systems that screen misaligned and dirty bags before packaging.
Implement Daily Tooling Maintenance
Scrub daily carbonized and caramelized sugar syrup, honey, and glycerin build-up from the hot sealing bars with non-abrasive brass brushes. Regular weekly testing for heater cartridge resistance and the thermocouple is important for detecting any indication of heating element wear.
Provide Proper Nitrogen Injection
To provide maximum shelf-life for premium shisha products, nitrogen should be injected into the package before sealing. Air exclusion during pouch holding period will guarantee preservation of molasses moisture content for 24 months shelf-life.
A properly maintained Premade Pouch Shisha Packaging Machine allows isolation of mechanical factors, thus guaranteeing freshness and absence of damage in the shipment.
3. Conclusion
Sealing integrity is the key factor that affects the brand reputation, flavor, and shelf life of the shisha packaging in today’s fiercely competitive international shisha industry. Running an efficient Premade Pouch Shisha Packaging Machine helps tobacco manufacturers to control their processes by keeping the optimal temperature conditions, balanced pneumatic pressure, and clean sealing surfaces even at the high speed of packaging.
If you experience problems with sealing, leaking of liquids, and contamination of shisha pouches while filling them, or if you consider implementing a modern automated packaging line at your manufacturing facility, please do not hesitate to reach out to our engineering department. Nargile Paketi will provide you with individualized Premade Pouch Shisha Packaging Machine designs, anti-drip dispensers, and turnkey factory solutions!